


In the rapidly expanding global commercial and industrial energy storage market, product stability, operational safety and long-term durability have become the core evaluation criteria for EPC contractors, project developers and industrial end-users. Many on-site operational failures of C&I energy storage systems stem from non-standard assembly, incomplete system debugging and insufficient pre-shipment performance tests. As a professional energy storage manufacturer with strict production management systems, MECC fully standardizes every production link. This article focuses on the on-site factory workflow of the 108KWH industrial and commercial energy storage cabinet, showcasing the complete standardized assembly, precise system debugging and multi-dimensional factory testing process, which fully demonstrates our reliable manufacturing strength and full-cycle quality assurance capabilities.
The 108KWH C&I energy storage cabinet is a mainstream compact integrated energy storage solution tailored for small and medium-sized commercial and industrial scenarios. Featuring flexible deployment, high space utilization and intelligent operation, this ESS cabinet is widely applied in office buildings, retail malls, small manufacturing factories and commercial parks. It effectively solves common industrial power pain points, including grid power instability, high peak electricity costs and insufficient emergency backup power. To ensure every delivered equipment can maintain long-term stable outdoor and indoor operation, MECC implements zero-tolerance production standards throughout the entire assembly and testing procedure, distinguishing our products from ordinary non-standard commercial energy storage equipment in the market.

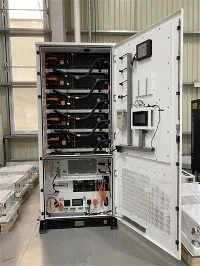
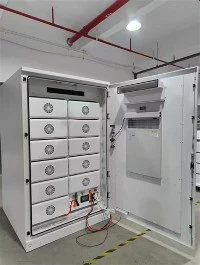
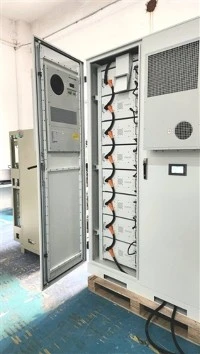
Standardized component assembly is the foundation of high-quality commercial energy storage cabinet production. Before formal assembly, our professional production team conducts strict screening and inspection for all raw materials and core components, including lithium battery modules, BMS circuit boards, EMS intelligent controllers, wiring harnesses, heat dissipation structures and fire protection accessories. Unqualified parts are strictly eliminated to avoid hidden dangers from the source. In the standardized dust-free workshop, workers complete modular installation in strict accordance with industrial production specifications. Every component is positioned accurately, and internal wiring follows unified layout standards with anti-short-circuit and anti-aging protection designs, ensuring neat wiring, stable signal transmission and safe electrical connection for the entire system.
After mechanical assembly is completed, systematic professional debugging becomes the key link to optimize system performance. Our technical team conducts comprehensive circuit and signal debugging to fully detect circuit connectivity, voltage stability and real-time signal transmission accuracy. Targeted calibration is performed on the built-in BMS battery management system to ensure precise monitoring of battery voltage, current and temperature data, realizing accurate overcharge and over-discharge protection. Meanwhile, we debug the EMS energy management system to verify intelligent functions such as automatic peak-valley switching, load adaptive adjustment and real-time energy scheduling, ensuring the system can flexibly respond to different commercial power consumption demands.
To guarantee adaptability and reliability in complex operating environments, the 108KWH ESS cabinet undergoes a complete set of strict factory testing procedures before shipment. The full charge and discharge cycle test is conducted to verify actual capacity accuracy and long-cycle operating stability, ensuring the product reaches standard energy storage efficiency. In addition, we simulate diverse ambient conditions through high and low temperature adaptation tests to confirm the system's stable operation in extreme temperature environments. All safety protection functions, including overvoltage, overcurrent, overheating and short-circuit protection, are triggered and tested repeatedly to eliminate potential safety risks. Finally, long-hour continuous load operation tests are carried out to check the overall coordination and stability of the integrated system.

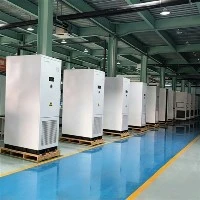
The standardized assembly, debugging and testing process fully reflects MECC's rigorousquality assurance system as a professional C&I energy storage manufacturer. Unified production standards ensure consistent quality of each batch of 108KWH energy storage cabinets, avoiding quality differences caused by irregular manual operation. Multi-layer testing and screening achieve zero-defect product delivery, greatly reducing on-site failure rates and later maintenance costs for overseas customers. Precise system debugging optimizes internal operation logic, effectively improving product cycle life and long-term operational stability, bringing sustainable and reliable energy-saving benefits for commercial and industrial projects.
FAQ
What is the complete production process of a 108KWH C&I energy storage cabinet?
The full workflow includes strict component inspection, standardized modular assembly, professional circuit and system debugging, charge-discharge cycle testing, environmental adaptation testing, safety function detection and final finished product qualification audit.
Why is factory debugging and testing essential for commercial ESS cabinets?
Professional debugging and testing eliminate assembly errors and potential safety hazards, optimize system operating parameters, and ensure long-term stable, safe and efficient operation of energy storage equipment in actual commercial scenarios.
What application scenarios suit the 108KWH industrial energy storage cabinet?
The compact 108KWH ESS cabinet is ideal for small and medium commercial buildings, offices, retail stores and small factories, supporting peak shaving, electricity cost reduction and emergency power backup.
Conclusion
The standardized assembly, precise debugging and strict factory testing of the 108KWH C&I energy storage cabinet fully showcase MECC's mature manufacturing technology and strict quality control system. Every production procedure follows international industrial standards, ensuring excellent safety, stability and durability of finished products. Adhering to customer-oriented and quality-first concepts, MECC continues to deliver high-quality, fully tested commercial and industrial energy storage equipment for global clients, providing reliable and cost-effective energy storage solutions for diverse small and medium-sized commercial energy transformation projects.